 en
 English
 中文简体
 русский
 Español
 عربى

Industry News
News & Blog
-
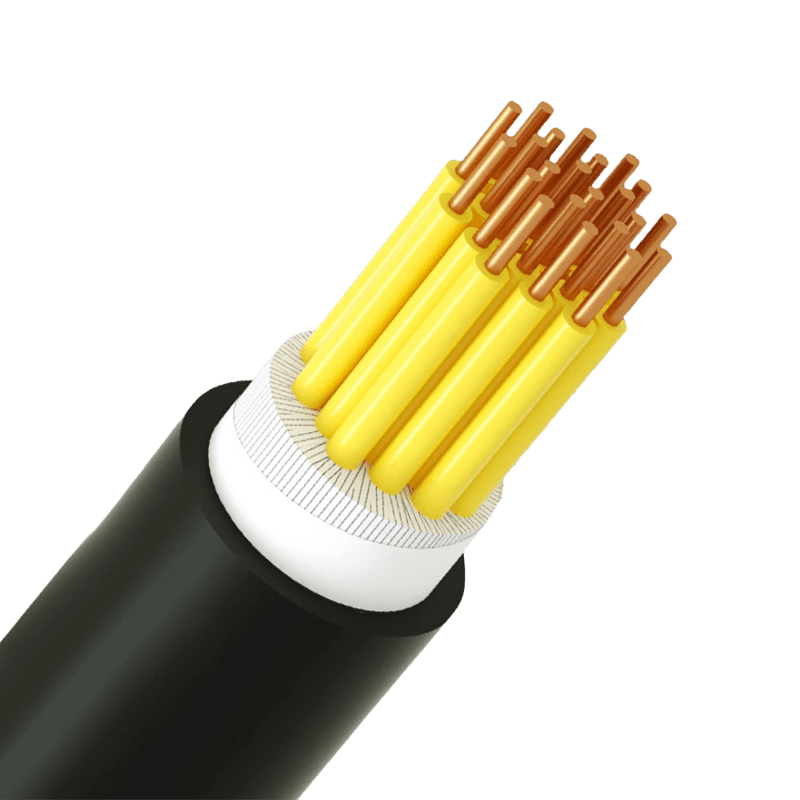 Copper Drawing Explained: From Rod Breakdown to Finished Cable ConductorA 2.5 mm² building wire and the 0.20 mm strand inside a robotic cable begin as the same object: an 8 mm copper rod. Between those two points sit a sequence of dies, lubricant tanks and annealing stages that most datasheets compress into two words, copper drawing. The same phrase turns up in art catalogues, where it means something else entirely: a copper point pressed across an abrasive ground, the metal cousin of silverpoint. The two meanings share a metal and nothing more. Here is the short answer before the detail. In cable manufacturing, copper drawing is a cold forming process that pulls copper rod through progressively smaller dies until the wire reaches the diameter, temper and surface finish a conductor needs. Get that stage right and stranding, insulation and final testing all behave. Get it wrong and the damage travels downstream as resistance failures, insulation faults and strands that crack at the terminal. What follows is the process, the numbers worth auditing, and the questions to ask before approving a conductor specification. Two Meanings, Two Industries Copperpoint Drawing in Art Metalpoint drawing uses a metal stylus on a ground coated with an abrasive preparation, usually gesso or a chalk-based mix. Silver and lead are the common styluses; copper, brass, bronze, gold and tin appear far less often because their lines are fainter and shift colour as the metal tarnishes. A copper point leaves a warm reddish-grey line that darkens over the years, so it suits underpainting, hatching and accents better than broad tonal passages. That line cannot be erased the way graphite can, which is why copperpoint drawings are built up stroke by stroke. Copper Wire Drawing in Cable Manufacturing Industrial drawing removes nothing and melts nothing. The copper is deformed: its cross-section shrinks, its length grows, and the crystal structure work-hardens, which is why the wire must be annealed before it can be stranded or bent around a terminal. A single line can turn 8 mm rod into 0.15 mm wire, a cross-sectional reduction of more than 99.9 percent. From Rod to Wire: The Drawing Sequence Most cable plants run the same six steps, whether the output is a rigid 2.5 mm² conductor or a flexible class 5 strand. Rod intake. Copper rod arrives at 8 mm diameter, typically Cu-ETP to EN 1977 or ASTM B49. Surface oxide and handling damage are removed first, because a contaminated rod surface becomes slivers later. Rod breakdown. The first machine pulls the rod through three or four tungsten carbide dies at high speed, cutting diameter to roughly 3 mm. Area reduction per pass is normally held between 15 and 25 percent. Intermediate drawing. Diameter drops into the 1.0 to 1.6 mm range. Cooling and lubricant filtration matter most here, since heat builds quickly as line speed rises. Fine and multi-wire drawing. Multi-wire machines draw up to 24 wires in parallel through synthetic diamond dies down to 0.15 to 0.5 mm, with individual tension control on each wire. In-line annealing. Resistance or inductive annealing restores elongation so the wire meets the ductility the conductor standard demands. Under-run this stage and strands crack during stranding. Tinning and spooling. An optional hot-dip or electroplated tin coating guards against oxidation, and the finished wire is wound onto bobbins matched to the strander. Numbers Worth Auditing on a Drawing Line Drawing is a stable process until a die wears, a lubricant drifts or an annealing contact ages. These are the parameters that move, and why each one matters downstream. Typical values for annealed plain copper conductors; confirm final limits against the IEC 60228 edition and the product standard named in your contract. Parameter Typical Value Why It Matters Input rod diameter 8 mm (some lines 12.5 mm) Sets the number of passes and how much surface must be cleaned Area reduction per die 15 to 25 percent Higher reduction risks wire breaks and slivers; lower reduction accelerates die wear Elongation, annealed copper 25 percent minimum for plain class 1 and 2 conductors Low elongation appears as cracked strands and failed bend tests DC resistance at 20 °C 1.5 mm²: 12.1 Ω/km; 2.5 mm²: 7.41 Ω/km; 4 mm²: 4.61 Ω/km A fast check that the drawn diameter is not running undersize Die material Tungsten carbide for coarse passes, synthetic diamond for fine Worn dies alter diameter and roundness mid-run Lubricant condition Emulsion or neat oil with monitored pH and conductivity Residue interferes with tinning, soldering and adhesion Notice that only one row concerns the drawing machine itself. The rest are about control: how much reduction each pass takes, how steadily the annealing stage holds, and how clean the wire leaves the line. Where Drawing Quality Shows Up in Finished Cable Conductor class is the clearest link between the drawing line and the cable you buy. IEC 60228 classes 1 and 2 cover solid and stranded conductors for fixed installation; classes 5 and 6 cover the flexible conductors used in control, appliance and robotic cables. A line that cannot hold diameter tolerance forces the strander to compensate, and that compensation usually surfaces as a resistance reading above the limit or a strand that snaps in a bend test. A rigid conductor for fixed installation inside a wall or conduit needs drawn, annealed wire that strands cleanly and holds its resistance per kilometre across the whole batch, because those terminations are made once and then hidden behind plaster or inside a panel. Drawing Defects and the Cost They Carry Downstream Drawing faults rarely stay on the drawing floor. They resurface at final test or, worse, in service. Wire breaks. Usually a reduction, lubricant or die geometry problem. Every break costs line time and leaves a spool that must be re-welded or scrapped. Slivers and copper fines. Loose particles pressed into the surface can thin insulation, showing up later as a spark test failure or an elevated partial discharge reading. Die wear. Diameter creep of a few micrometres is enough to push a conductor outside its resistance limit over a long run. Poor elongation. Under-annealed wire cracks during stranding, and the crack often becomes visible only after the insulation is stripped. Surface oxidation. Tarnish blocks wetting during soldering and weakens tin adhesion. Tinning is the usual answer to oxidation, but it changes the conductor in ways worth understanding before it goes into a specification, from slightly higher resistance per kilometre to different behaviour at the terminal. Comparing tinned and bare copper conductors is a better starting point than copying whatever option appeared on the last project's bill of materials. Specifying by Conductor, Not by Process Buyers do not purchase a drawing process; they purchase the conductor behaviour that process produces. Five questions settle most of it. Which conductor class does the installation and its standard require: class 1, 2, 5 or 6? What is the maximum DC resistance at 20 °C for the cross-section, and is it stated in the standard or only in the datasheet? Is plain or tinned copper required by the environment, the operating temperature and the termination method? How many strands, and what is the nominal strand diameter? Which standard governs: IEC 60228 alone, or a product standard such as IEC 60502 or IEC 60227 on top of it? In industrial automation those questions usually resolve into a flexible multicore cable with class 5 copper, screened or unscreened, sized for the drive and the cable tray route. Control Cables ManufacturersPlastic Insulated Control CableView Product → For distribution circuits the same logic runs at a larger scale, where stranded class 2 copper, XLPE insulation and a defined resistance limit matter more than strand count. Low Smoke Halogen Free Fire Resistant Low-Voltage Power Cable Manufacturers0.6/1kV Cross-Linked Polyethylene/PVC Insulated Power CableView Product → Questions for a Cable Supplier About Their Drawing The answers tell you how much of the conductor is under the supplier's control and how much depends on an outside wire mill. Is the wire drawn in house, and how many drawing lines are running? Is annealing in line with drawing, or handled on a separate machine? Are elongation and resistance checked per batch or per spool? Are rod heat numbers traceable through to the finished cable drum? What spark test voltage is applied after insulation? A walk through the drawing hall answers several of those faster than a questionnaire. When rod intake, drawing, annealing and extrusion sit under one roof, conductor defects are caught before insulation rather than after shipment. You can see how that layout works on the factory page, and match the conductor classes described there against the five questions above. Copper drawing sits at the start of nearly every cable conversation, and it is easy to treat as a commodity step. It is not. The diameter, temper and surface of the drawn wire set the ceiling for how the finished cable performs in a wall, a tray or a moving machine, and no amount of insulation or final testing recovers what the drawing line gave away. Treat the conductor specification as the controlling document, ask for the resistance and elongation figures behind it, and the cable you receive will match the cable you specified. .article-section{margin-bottom:24px;border-bottom:1px solid #fde9db;padding-bottom:20px;} .article-section:last-of-type{border-bottom:none;padding-bottom:0;} .article-section:first-of-type{background-color:#fde9db;border-left:4px solid #f1760c;border-bottom:none;padding:18px;} .article-section h2{font-size:22px;font-weight:bold;text-align:left;margin-bottom:12px!important;border-left:4px solid #f1760c;padding-left:10px;color:#333333;} .article-section h3{font-size:16px;font-weight:bold;text-align:left;margin-bottom:12px;color:#f1760c;} .article-section p{font-size:16px!important;margin-bottom:12px;} .article-section ol{margin-bottom:12px;list-style-type:decimal;list-style-position:inside;padding-left:0;} .article-section ul{margin-bottom:12px;list-style-type:disc;list-style-position:inside;} .article-section li{list-style:inherit;font-size:16px;margin-bottom:6px;} .article-section table{display: table!important;width:100%;border-collapse:collapse;margin-bottom:12px;} .article-section thead{display: table-header-group!important;background-color:#fde9db;} .article-section tbody{display: table-row-group!important;} .article-section tr{display: table-row!important;} .article-section th{display: table-cell!important;font-weight:bold;border:1px solid #cccccc;padding:8px;} .article-section td{display: table-cell!important;border:1px solid #cccccc;padding:8px;text-align: center;} .article-section caption{caption-side:bottom;font-size:16px;margin-bottom:12px;font-style:italic;color:#808080;} .product-card{display:block;margin:20px 0;border:1px solid #e5e7eb;border-radius:10px;overflow:hidden;font-style:normal;background:#fff} .pc-inner{display:flex;text-decoration:none;color:inherit;align-items:center;min-height:120px} .pc-img{width:160px;min-width:160px;aspect-ratio:4/3;height:auto;min-height:120px;object-fit:cover;flex-shrink:0;display:block;align-self:stretch} .pc-body{padding:12px 16px;flex:1;min-width:0;display:flex;flex-direction:column;align-self:stretch;justify-content:center} .pc-title{display:block;font-size:15px;font-weight:600;color:#111;margin:0 0 6px;line-height:1.4} .pc-desc{display:-webkit-box;font-size:13px;color:#6b7280;margin:0 0 8px;line-height:1.5;overflow:hidden;-webkit-line-clamp:2;line-clamp:2;-webkit-box-orient:vertical} .pc-cta{display:block;font-size:13px;font-weight:600;color:inherit;margin-top:auto} .pc-inner:hover .pc-title{text-decoration:underline} .article-section a:not(.pc-inner),article a:not(.pc-inner){color:inherit}.pc-cta{color:inherit!important}
-
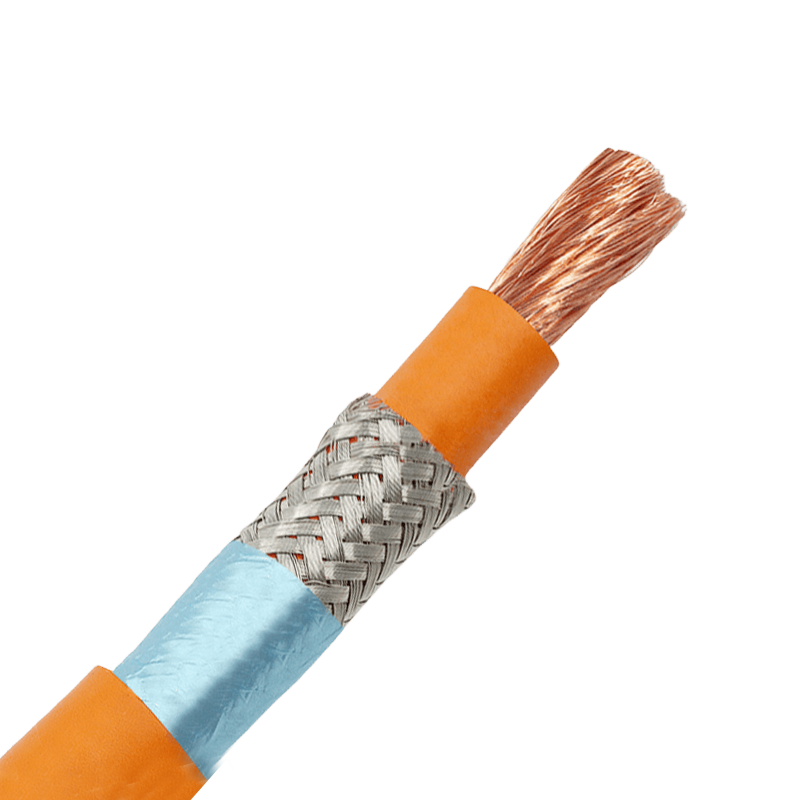 What Is Thermoplastic Rubber (TPR)? Properties, Uses & Cable ApplicationsPick up a portable power cord on a cold morning and you can usually tell what its sheath is made of within seconds. A plasticized PVC jacket tends to feel stiff and hold the shape it was coiled into overnight, while a rubbery jacket springs back and stays supple close to freezing. That rubbery hand-feel, common in modern cords, tool cables, and molded grips, comes from thermoplastic rubber, abbreviated TPR. In brief: thermoplastic rubber is a family of materials that behaves like cured rubber in service yet melts and re-forms like plastic during manufacturing. The sections below explain how that dual behavior works, how TPR compares with vulcanized rubber and PVC, where it fits in cable construction, and which numbers to check before specifying it. What Is Thermoplastic Rubber (TPR)? Thermoplastic rubber is the trade name for what engineers call a thermoplastic elastomer (TPE). It is not a single polymer but a family of copolymers and blends built from two phases: hard plastic segments that soften when heated, and soft rubbery segments that provide elasticity. In short, TPR delivers rubber performance through plastic processing. Hard domains (physical crosslinks) Soft rubbery matrix Below its softening range, the hard phase locks the soft phase in place and works as a set of physical crosslinks, so the material stretches and recovers like rubber. Heat it above that range and the links disengage, letting the compound flow through an extruder or injection molding machine; cool it and the rubbery state returns. In raw form TPR is typically a translucent or milky-white pellet that runs on standard thermoplastic equipment, with no curing ovens and no sulfur. Commercial grades fall into five broad families, and the family behind the label matters more than the label itself: Table 1. The five major TPR families and typical property ranges; exact values depend on the compound. Family Base chemistry Typical hardness Typical continuous service temperature Common uses Styrenic (SBS, SEBS) Styrene block copolymers, often blended with polypropylene and oils Shore 10A to 65D About -50 to +90 °C Grips, seals, footwear, cable jackets TPV Fine EPDM rubber particles cured inside a polypropylene matrix Shore 35A to 50D Up to about +125 °C Weather seals, under-hood parts, cable jackets TPU Thermoplastic polyurethane Shore 60A to 74D About -40 to +100 °C Abrasion-resistant jackets, hoses, films TPO Polypropylene blended with EPDM rubber Shore 60A to 75D About -40 to +100 °C Automotive fascias, roofing membranes Copolyester (TPEE) Polyester hard segments with polyether soft segments Shore 35D to 72D About -40 to +110 °C Gears, bellows, hydraulic hose How TPR Differs from Vulcanized Rubber and PVC The defining difference is chemistry. Conventional rubber becomes elastic through vulcanization, an irreversible chemical crosslinking reaction; TPR relies on reversible physical crosslinks; flexible PVC gains softness from plasticizers. Each route produces a distinct property profile. Table 2. Practical comparison of the three material options used for flexible cable jackets and insulation. Property Thermoplastic rubber (TPR) Vulcanized rubber Flexible PVC Processing Melt-processable, no curing step Requires vulcanization with heat and curing agents Melt-processable Production scrap Usually reground and reused Cannot be re-melted Usually reprocessed Low-temperature flexibility Good to excellent, often to -40 °C Excellent Moderate; stiffens in cold unless specially compounded Continuous heat resistance Moderate; most grades hold between about 90 and 125 °C High; many compounds rated 105 to 150 °C and above Moderate; typically 70 to 90 °C Compression set Higher; recovers less under sustained pressure Low; recovers well Moderate to high Weathering and ozone Good for SEBS and TPV; SBS degrades in UV Good, especially EPDM Good with additives; plasticizer migration possible Relative cost Moderate; offset by shorter cycles and scrap reuse Higher processing cost Lowest Two practical consequences follow. Cured rubber needs minutes of dwell in a vulcanization line, while TPR solidifies as soon as it cools, and its trimmed scrap can go straight back into the machine. TPR also bonds well to rigid thermoplastic substrates in two-shot molding, which is why connector strain reliefs, tool grips, and cable glands are so often overmolded in one pass. Where TPR Earns Its Place in Cable Design In the cable industry, TPR competes directly with flexible PVC and vulcanized rubber for jackets on products that move, flex, and get handled. Typical applications include: Power tool and appliance cords that need a dry, grippy surface and cold-weather workability Welding and battery cables routed across workshop floors Robot and drag-chain cables subject to millions of flex cycles EV charging cable jackets dragged over concrete and handled in winter Overmolded connector strain reliefs and molded plugs For household and workshop cords, a TPE or rubber-family sheath keeps the cable workable in cold garages and on building sites, where plasticized PVC would feel stiff and kink. Our rubber-sheathed flexible cables cover the H07BZ-F and YC-type constructions where this behavior is specified. Rubber-Sheathed Flexible Cables for Portable PowerThese rubber insulated and sheathed flexible cables offer excellent cold flexibility, oil and abrasion resistance, and waterproofing. They suit the H07BZ-F and YC-type cords mentioned for cold garages, building sites, and portable equipment.View Product → EV charging has become one of the strongest growth areas for TPE jacket materials. The compounds stay flexible at low ambient temperatures, resist abrasion from daily handling, and bond cleanly to overmolded strain reliefs. Our EV charging cables are built around exactly these requirements. EV Charging Cables with TPE Jacket PerformanceBuilt for charging pile applications, these EV charging cables provide strong weather resistance, oil and wear resistance, and heat tolerance during charging, matching the TPE jacket qualities described for outdoor EV charging environments.View Product → Choosing between PVC, TPE, and rubber for a given cord is rarely about one property; it is a balance of cold flexibility, oil exposure, outdoor weathering, flame requirements, and price. Our guide to electrical equipment cable types and materials walks through that decision step by step. When TPR Is Not the Right Choice TPR's physical crosslinks are heat-reversible, and that is also its ceiling. As continuous temperatures approach a grade's rating, the material softens gradually and creep under clamps, cable ties, and sustained loads rises sharply. Applications that need dimensional stability at elevated temperatures, such as solar DC wiring, use chemically crosslinked compounds instead; our article on crosslinking degree and heat deformation in PV cables explains why that curing step matters. The same logic applies to fixed building and infrastructure wiring, where cold flexibility is a minor benefit and thermal endurance dominates. Crosslinked XLPE insulation remains the standard choice there, as in our 0.6/1 kV XLPE insulated power cables. YJV22 0.6/1kV XLPE Insulated Armoured Power CableThis 0.6/1 kV XLPE insulated, steel tape armoured cable with copper conductors and PVC sheath suits fixed distribution where thermal endurance and mechanical protection matter, as described for building and infrastructure wiring.View Product → A Six-Point Checklist Before You Specify Before approving any TPR compound, work through this checklist: Identify the base family (SEBS, TPV, TPU, TPO, or copolyester), since weathering and temperature capability follow from it. Request Shore hardness on both the A and D scales, because a single number can hide a wide range of feel and crush resistance. Match the low-temperature rating to the worst installation case, not the average one. Compare the continuous operating temperature with your real duty cycle, including heat generated inside cable bundles. Confirm flame-retardant and halogen-free grades against the standard your project cites. Ask for material data sheets and cable test reports rather than accepting the generic TPR label. Thermoplastic rubber is best understood as rubber performance delivered through plastic processing: two-phase materials whose physical crosslinks provide elasticity in service and release under heat, making TPR fast to manufacture, colorable, overmoldable, and largely recyclable. That combination explains why it has become the default for soft grips, cold-flexible cords, and EV charging jackets, while vulcanized rubber and crosslinked polyolefins keep the jobs that demand higher heat endurance. For buyers, the practical step is to identify the family behind the TPR label, then match hardness, temperature window, weathering, and flame performance to the actual duty cycle of the cable or part. .article-section{margin-bottom:32px;} .article-section h2{font-size:22px;font-weight:bold;text-align:left;margin-bottom:12px!important;color:#c25508;border-bottom:2px solid #f1760c;padding-bottom:8px;} .article-section h3{font-size:16px;font-weight:bold;text-align:left;margin-bottom:12px;color:#c25508;} .article-section p{font-size:16px!important;margin-bottom:12px;line-height:1.7;} .article-section ol{margin-bottom:12px;list-style-type:decimal;list-style-position:inside;padding-left:0;} .article-section ul{margin-bottom:12px;list-style-type:disc;list-style-position:inside;} .article-section li{list-style:inherit;font-size:16px;margin-bottom:6px;line-height:1.6;} .article-section table{display: table!important;border-collapse:collapse;width:100%;margin-bottom:12px;} .article-section thead{display: table-header-group!important;} .article-section tbody{display: table-row-group!important;} .article-section tr{display: table-row!important;} .article-section th{display: table-cell!important;font-weight:bold;border:1px solid #cccccc;padding:8px;background:#fde9db;color:#8a4212;} .article-section td{display: table-cell!important;border:1px solid #cccccc;padding:8px;text-align: center;} .article-section table caption{caption-side:bottom;font-size:16px;margin-bottom:12px;font-style:italic;color:#808080;} .article-section a{color:#e07008;text-decoration:none;} .article-section a:hover{text-decoration:underline;} .article-section a[data-product-card="true"]{display:inline-block;background:#fde9db;border:1px solid #f1760c;border-radius:8px;padding:8px 18px;margin:2px 0 16px;color:#c25508;font-weight:bold;text-decoration:none;} .article-section a[data-product-card="true"]:hover{background:#f1760c;color:#ffffff;text-decoration:none;} .product-card{display:block;margin:20px 0;border:1px solid #e5e7eb;border-radius:10px;overflow:hidden;font-style:normal;background:#fff} .pc-inner{display:flex;text-decoration:none;color:inherit;align-items:center;min-height:120px} .pc-img{width:160px;min-width:160px;aspect-ratio:4/3;height:auto;min-height:120px;object-fit:cover;flex-shrink:0;display:block;align-self:stretch} .pc-body{padding:12px 16px;flex:1;min-width:0;display:flex;flex-direction:column;align-self:stretch;justify-content:center} .pc-title{display:block;font-size:15px;font-weight:600;color:#111;margin:0 0 6px;line-height:1.4} .pc-desc{display:-webkit-box;font-size:13px;color:#6b7280;margin:0 0 8px;line-height:1.5;overflow:hidden;-webkit-line-clamp:2;line-clamp:2;-webkit-box-orient:vertical} .pc-cta{display:block;font-size:13px;font-weight:600;color:inherit;margin-top:auto} .pc-inner:hover .pc-title{text-decoration:underline} .article-section a:not(.pc-inner),article a:not(.pc-inner){color:inherit}.pc-cta{color:inherit!important}
-
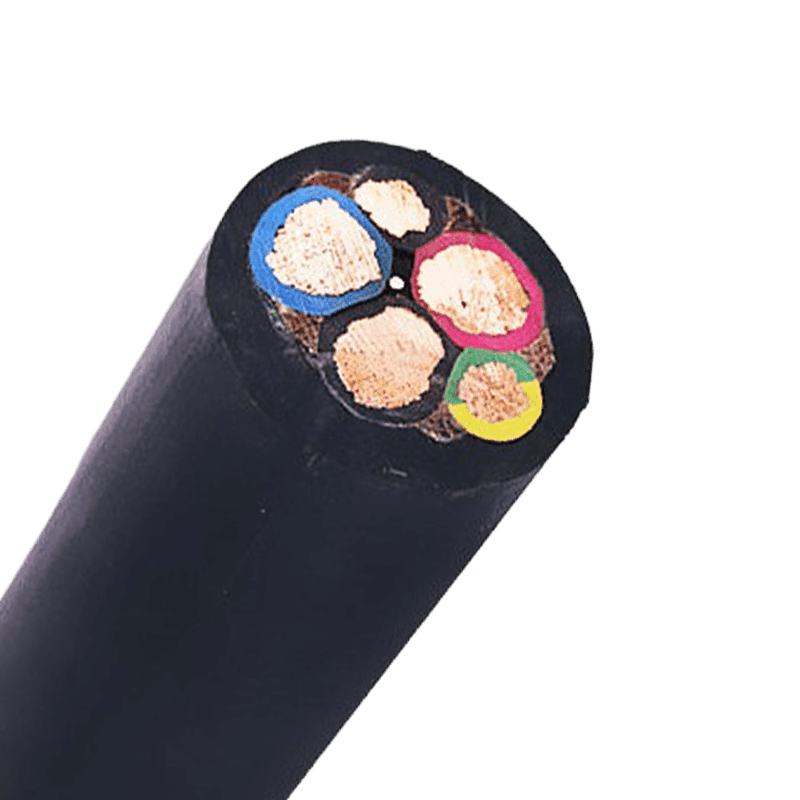 Cable Strain Relief in Practice: Construction, Installation and SelectionA cable that looks perfectly fine from the outside can still fail internally. Strip the jacket near a terminal box and you may find conductors pulled away from their crimps, with insulation showing white stress marks at the bending point. This is the classic signature of strain damage. It rarely appears on the day of installation; it develops over months of vibration, thermal cycling, and the occasional careless tug. Once mechanical pull reaches the conductor and its termination, no jacket material can stop the eventual open circuit. In production environments, this type of failure shows up as a sudden machine stop, an error code on a drive, or an intermittent signal that is nearly impossible to trace. What Cable Strain Relief Actually Does Strain relief is a simple mechanical concept: shift the pulling force away from the weakest point and onto a part of the assembly designed to take it. In any cable installation the weakest points are the solder joints, crimped terminals, and the boundary where the cable enters a housing. The strongest points are the cable sheath, internal braids, and rigid structural elements such as enclosures or brackets. A properly designed strain relief system clamps or supports the cable sheath so that any pull is absorbed by the sheath and transmitted to the enclosure, not to the electrical connection. Why is this separation of forces so important? Copper conductors are ductile. A tensile load that seems small — only a few kilograms — can gradually elongate the conductor, reduce its cross-section, and create a hot spot. In stranded construction, individual wires break one by one. The terminal then carries the remaining load, and eventually the whole termination fails. Strain relief prevents this chain of events by keeping the conductor mechanically unloaded. A good strain relief design also protects the cable from the environment. The clamp point is often the only place where moisture, dust, and solvent fumes can enter the interior of a cable. A compression-type fitting with a proper seal does double duty as a gland and an ingress barrier. That is one reason why the strain relief fitting and the cable jacket must be considered together, not as separate items. Cable Construction Factors That Affect Strain Relief Not all cables behave the same way under pull stress. The construction of the cable determines how much load is absorbed by the sheath and how much reaches the conductors. When you are selecting a cable for a demanding installation, examine four elements: jacket material, conductor stranding, reinforcement layer, and overall flexibility. Cable construction features that help or hurt strain tolerance Construction Feature Effect on Strain Relief Typical Applications Thick PVC jacket Distributes clamp pressure well General industrial wiring Rubber jacket (EPR or neoprene) High surface grip, resists cutting at the clamp Portable tools, machine wiring Class 5 flexible conductors Reduce internal friction under bending Control panels, robotics Metal braid or armour Carries tension directly if correctly clamped Medium voltage, industrial plants Among these, the jacket material has the greatest influence at the strain relief point. A cable gland or clamp grips the outer surface of the jacket. A soft PVC jacket can be permanently deformed by the clamp, which reduces grip over time and lets the cable slide. Rubber jackets hold their compression set better and keep the cable firmly gripped without being cut. That is why portable and machine-tool cables usually use rubber-sheathed constructions. Flexibility is not a luxury. In applications where the cable flexes continuously, stiff conductor stranding will fatigue at the clamp point regardless of the jacket. Class 5 flexible conductors distribute the movement across a larger number of fine wires, so each wire sees less stress. The IEC 60228 classification gives you a straightforward way to specify the right stranding for the movement profile of your machine. Three Practical Ways to Keep Pull Stress Off Terminals You can solve most strain relief problems in three ways: clamp the sheath at the entry point, route the cable so that natural forces work with you, and protect the cable in high-motion zones. 1. Clamp the sheath at the entry point Use a cable gland, grommet, or strain relief bushing where the cable enters an enclosure. The fitting must match the outer diameter of the cable closely. A loose gland that fits a broader OD range will grip unevenly and can pull away over time. Anchor the fitting on a rigid wall, not on a thin removable panel. 2. Route cables so the pull direction is neutral Cable should enter from below or from a direction that lets gravity and the cable's own weight aid the connection, not work against it. Avoid pulling the cable taut between fixing points. If a length must run horizontally over a long distance, support it with intermediate clamps so the weight does not hang on the terminal. 3. Add spring guards, flexible conduit, or spiral wrap in moving zones Machines that rotate, slide, or vibrate put repeated bending stress on a cable at the point where it is clamped. A spring guard or a short length of flexible conduit takes up the movement and prevents the bend radius from dropping below the cable's minimum. This also protects the clamp from permanent loosening over time. These mechanical measures are easy to apply and inexpensive, but they only work if the cable jacket can withstand clamping force over years of service. The practical guidance on PVC-sheathed flexible cable selection and installation covers exactly this type of decision for ordinary industrial environments. Selecting Cables for Environments With High Pull Stress The right cable construction makes strain relief easier and more reliable. For portable equipment and frequent flexing, start with a rubber-sheathed cable. The jacket grips fittings better, tolerates repeated bending, and maintains its shape at the clamp point far longer than a standard PVC jacket. A rubber-sheathed cable is the safer choice for hand tools, test equipment, and temporary power supplies, where users drag the cable across floors and pull on it without thinking about the terminal. Rubber-Sheathed Flexible Cable for Portable Equipment and ToolsThis rubber-insulated and sheathed cable is built for frequent flexing and rough handling. Its oil, abrasion, and water resistance suit portable power tools, cranes, and temporary supplies, making it a practical option for the strain-relief concerns discussed earlier.View Product → In control cabinets and automation systems, a plastic-insulated multicore control cable is a common choice. These cables use flexible conductors and a smooth outer sheath that seats well inside cable ducts and glands. They are designed for low-voltage control circuits, instrumentation, and signal connections where terminal reliability matters. The choice of stranding class and sheath thickness directly affects how the cable behaves at the strain relief point. Our control cable selection guide outlines the features to check before ordering. Plastic-Insulated Multicore Control Cable for Low-Voltage SystemsDesigned for control, signal, and measurement circuits up to 450/750V, this cable offers good insulation, multiple core options, and interference resistance. It fits the control cabinet and automation context where terminal reliability and duct seating are priorities.View Product → Variable frequency drive installations deserve a special mention. The cable between a VFD and a motor is exposed both to continuous vibration and to voltage reflection from the drive output. A standard power cable may work for a while, but it is not designed for the combination of mechanical stress and harmonic stress that a drive system produces. A dedicated VFD cable with a symmetric grounded conductor keeps termination points quiet and reduces the risk of long-term insulation damage. If the cable runs through a conduit and is pulled hard during installation, the more robust symmetrical construction of a VFD cable also makes it easier to handle without distorting the core geometry. Symmetrical VFD Cable with Shielding for Drive InstallationsThis variable frequency drive supply cable handles voltage surges, frequency pulses, and electromagnetic interference. Its robust construction suits the vibration and harmonic stress between a VFD and motor, and it withstands high conductor temperatures up to 90°C.View Product → How to Verify Strain Relief During Installation After the cable is terminated, do a few simple checks before closing the panel: Pull on the cable at the entry point and confirm that the sheath, not the conductor, takes the load. If the terminal moves when you pull the cable, the strain relief is not working. Measure the bend radius at every turn. A tight 90-degree bend immediately behind a gland is a common source of conductor fatigue. Look at how the cable is fixed along its path. Use intermediate clamps at intervals recommended by the manufacturer or supplier. For outdoor or washdown areas, install a drip loop so water cannot travel along the cable and enter the enclosure. These checks take less than a minute each and cost nothing, yet they eliminate the most frequent causes of premature termination failure. Effective strain relief is not a single accessory. It is a system that combines the right cable construction, the right entry fitting, and a routing plan that respects bending limits. When these three pieces are aligned, the weakest point of a cable assembly stops being the terminal connection. .article-section caption{caption-side:bottom;font-size:16px;margin-bottom:12px;font-style:italic;color:#808080;} .article-section table{display:table!important;} .article-section thead{display:table-header-group!important;} .article-section tbody{display:table-row-group!important;} .article-section tr{display:table-row!important;} .article-section th{display:table-cell!important;font-weight:bold;border:1px solid #cccccc;padding:8px;} .article-section td{display:table-cell!important;border:1px solid #cccccc;padding:8px;text-align:center;} .article-section ol{margin-bottom:12px;list-style-type:decimal;list-style-position:inside;padding-left:0;} .article-section ul{margin-bottom:12px;list-style-type:disc;list-style-position:inside;} .article-section li{list-style:inherit;font-size:16px;margin-bottom:6px;} .article-section h2{font-size:22px;font-weight:bold;text-align:left;margin-bottom:12px!important;} .article-section h3{font-size:16px;font-weight:bold;text-align:left;margin-bottom:12px;} .article-section p{font-size:16px!important;margin-bottom:12px;} .product-card{display:block;margin:20px 0;border:1px solid #e5e7eb;border-radius:10px;overflow:hidden;font-style:normal;background:#fff} .pc-inner{display:flex;text-decoration:none;color:inherit;align-items:center;min-height:120px} .pc-img{width:160px;min-width:160px;aspect-ratio:4/3;height:auto;min-height:120px;object-fit:cover;flex-shrink:0;display:block;align-self:stretch} .pc-body{padding:12px 16px;flex:1;min-width:0;display:flex;flex-direction:column;align-self:stretch;justify-content:center} .pc-title{display:block;font-size:15px;font-weight:600;color:#111;margin:0 0 6px;line-height:1.4} .pc-desc{display:-webkit-box;font-size:13px;color:#6b7280;margin:0 0 8px;line-height:1.5;overflow:hidden;-webkit-line-clamp:2;line-clamp:2;-webkit-box-orient:vertical} .pc-cta{display:block;font-size:13px;font-weight:600;color:inherit;margin-top:auto} .pc-inner:hover .pc-title{text-decoration:underline} .article-section a:not(.pc-inner),article a:not(.pc-inner){color:inherit}.pc-cta{color:inherit!important}
-
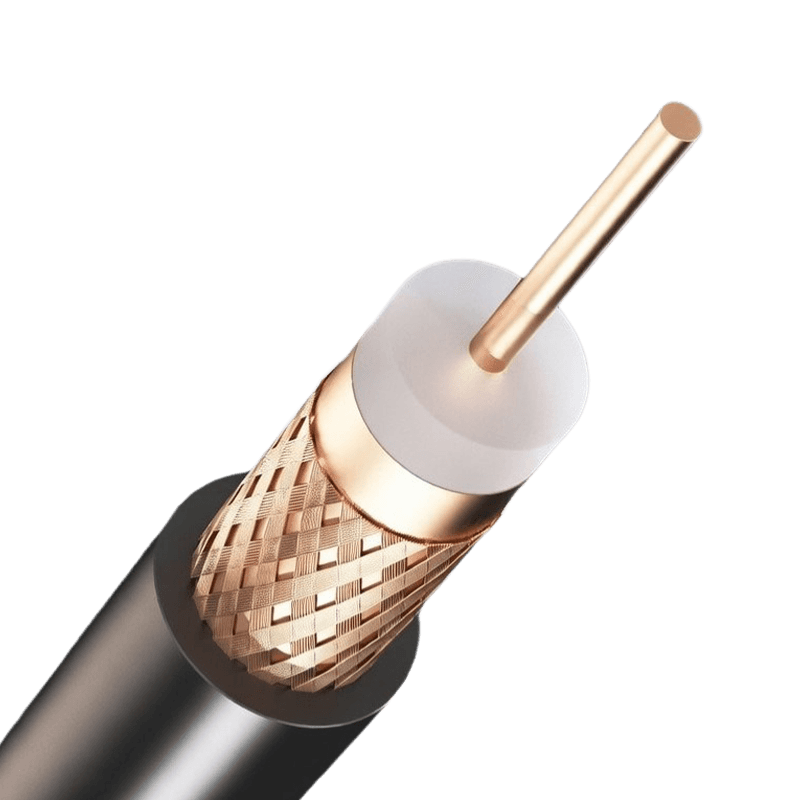 Oxygen Free Copper (OFC): Grades, Properties, and When It Really MattersTwo reels of copper conductor can sit side by side in a warehouse and look identical, yet one was melted and cast without ever touching air, while the other carries up to 400 ppm of oxygen locked inside as copper oxide particles. That single difference defines oxygen free copper (OFC): a grade of copper with oxygen content at or below 0.001% (10 ppm), copper purity of 99.95% or higher, and a casting route that keeps the melt sealed away from the atmosphere. The conclusion up front: OFC delivers measurable value in hydrogen atmospheres, vacuum systems, cryogenic equipment, and precision signal cables, and it is usually an unnecessary cost in general power distribution and building wiring. Knowing which side of that line a project falls on is what separates a sound specification from a padded budget. What Oxygen Free Copper Means on a Datasheet When a supplier calls copper oxygen free, the term points to standardized grades rather than a marketing mood. The two most common designations should appear by name on any purchase order: Cu-OF (UNS C10200): oxygen content no greater than 0.001%, with copper purity of at least 99.95% Cu-OFE (UNS C10100, often labeled oxygen-free electronic copper): oxygen content no greater than 0.0005%, with purity of 99.99% or better Both grades are covered by ASTM B170 in the United States and EN 13601 in Europe. The baseline for comparison is electrolytic tough pitch copper (ETP, UNS C11000), which represents the overwhelming majority of copper produced worldwide. ETP is cast in contact with air, and a controlled oxygen level of roughly 0.02% to 0.04% is deliberately left in the melt because it scavenges impurities during refining. That oxygen is harmless in most service conditions, which is exactly why ETP dominates commodity applications. Typical specification limits for common copper conductor grades under ASTM and UNS designation systems. Grade UNS Number Oxygen Content Copper Purity Minimum Conductivity Electrolytic tough pitch (ETP) C11000 0.02-0.04% (200-400 ppm) 99.90% min 100% IACS Oxygen-free copper (Cu-OF) C10200 0.001% max (10 ppm) 99.95% min 100% IACS Oxygen-free electronic (Cu-OFE) C10100 0.0005% max (5 ppm) 99.99% min 101% IACS The figures above explain a recurring purchasing question: if ETP and Cu-OF are both rated at 100% IACS, what does the extra money actually buy? The answer lies in process-dependent properties rather than headline conductivity, which the next sections address. How the Manufacturing Process Removes the Oxygen Oxygen free copper is not made by refining tough pitch copper an extra step. It starts from the same electrolytic cathode but takes a fundamentally different casting route. The cathode is melted in an induction furnace sealed under a reducing or inert atmosphere, typically carbon monoxide or nitrogen, so oxygen never dissolves into the melt in the first place. Upward continuous casting, known in the industry as the Upcast process, then pulls solid rod directly out of the molten pool through a graphite die, keeping the metal shielded from air until it has fully solidified. The result is a microstructure free of copper oxide particles at the grain boundaries. In practice this shows up as cleaner drawing behavior: fewer inclusions mean fewer break points when reducing down to fine and ultra-fine gauges, and a more uniform annealing response from batch to batch. For a cable manufacturer, that consistency is a production advantage before any end-user property is even considered. The Properties That Justify the Premium Hydrogen embrittlement resistance This is the decisive property. In tough pitch copper, copper oxide (Cu2O) dispersed along the grain boundaries reacts with hydrogen at elevated temperatures, roughly 370°C and above, forming high-pressure steam inside the metal. That steam opens internal fissures and can crack a component outright during hydrogen furnace brazing, annealing in hydrogen atmospheres, or long service in hydrogen-rich environments. Oxygen free copper contains no oxide phase, so it is effectively immune to this failure mode. That is why OFC is the default requirement for brazed assemblies, vacuum furnace hardware, and equipment destined for hydrogen service. Conductivity at the ceiling Both ETP and Cu-OF carry a minimum rating of 100% IACS, while Cu-OFE can reach 101%. A one percent gain sounds trivial, and for a 50-meter power feeder it genuinely is. It becomes meaningful in precision resistors, calibration-grade conductors, and very long signal runs where every increment of resistivity compounds along the length. Ductility and microstructural cleanliness With no oxide inclusions, OFC forms more predictably in deep drawing, flaring, and glass-to-metal sealing, and it draws into fine wire with lower break rates. These properties matter most to component makers, though cable producers drawing fine stranding benefit from the same cleanliness. Where OFC Earns Its Cost and Where It Does Not Applications that depend on it Vacuum technology and hydrogen service top the list. Waveguides, particle accelerator components, vacuum furnace fixtures, and brazed assemblies all depend on the embrittlement resistance described above. Cryogenic systems specify OFC because its thermal conductivity holds up better at low temperatures than that of oxide-bearing grades, which matters for superconducting magnet leads, medical imaging coils, and plasma-facing components. Signal transmission is the largest cable-side market. High-grade RF coaxial assemblies are routinely built on oxygen free copper because conductor surface quality influences high-frequency behavior: at radio frequencies, current crowds toward the conductor surface, so surface anomalies have an outsized effect. Audio interconnects, instrumentation circuits, and precision measurement leads follow the same reasoning. Coaxial Cables for Stable High-Frequency Signal TransmissionBuilt with accurate impedance matching, strong shielding, and a bending radius of no more than ten times the outer diameter, these coaxial cables suit the RF and instrumentation circuits discussed above, where conductor surface quality directly affects high-frequency performance.View Product → The same logic extends to low-level signal circuits in factories and data rooms, where instrument loops leave little margin for conductor inconsistency. Computer and Instrumentation Cables for Low-Level SignalsThese 300/500 V PE-insulated cables offer low signal distortion, high transmission rates, and strong electromagnetic interference resistance, making them well suited to the factory and data-room instrument loops where conductor consistency leaves little margin for error.View Product → Readers planning signal infrastructure can see how conductor, shielding, and jacket decisions fit together in our communication and data industry overview. Where standard copper is the smarter choice Building wire, low-voltage power cable, and most medium-voltage distribution run on tough pitch copper by design. Standards such as IEC 60228 and ASTM B3 define resistivity, elongation, and dimension requirements that ETP meets at its standard price point, and oxygen content has no bearing on ampacity, insulation life, or terminations in ordinary service. Paying an OFC premium in these applications buys nothing measurable. What does matter is conductor construction, from solid class 1 cores to flexible class 5 stranding, and, in corrosive or marine environments, whether the conductor should be tin-plated. We cover that plating decision separately in our comparison of tinned copper versus bare copper conductors. Copper Building Wires for 450/750V Electrical SystemsPVC and XLPE insulated building wires rated 450/750V and below cover a full range of diameters for different loads. For ordinary power distribution, standard tough pitch copper meets IEC and ASTM requirements without paying an OFC premium.View Product → Verifying the Grade Before the Purchase Order Because OFC appears on packaging far more often than it is actually tested, verification should be contractual rather than assumed. A credible oxygen free copper offer includes: A mill test certificate stating the UNS grade (C10200 or C10100) and heat-lot chemical composition. Oxygen analysis by inert gas fusion, with the ppm value reported rather than merely claimed. Resistivity testing per ASTM B193, since conductivity is the property certification will be judged on. For hydrogen service, results from a hydrogen embrittlement acceptance test following annealing. Two clarifications prevent common purchasing mistakes. First, copper grade and conductor class are separate variables: IEC 60228 classes 1 through 6 describe stranding and flexibility, not oxygen content, so a class 5 flexible conductor can be either ETP or OFC. Second, oxygen free does not mean corrosion-proof; outdoor and marine durability depend far more on insulation, sheathing, and plating choices than on residual oxygen content. Oxygen free copper is best treated as an engineering answer to specific environments, including hydrogen exposure, vacuum, cryogenics, and precision signal paths, rather than a universal upgrade. Specifying it where those conditions exist prevents a well-understood failure mode; specifying it everywhere else inflates cost without changing performance. As a cable manufacturer producing power, control, communication, and specialty cables for customers worldwide, we work with both standard tough pitch and higher-purity conductors and can help match the grade to the service environment. If a project sits on the line between the two, our engineering team can review the operating conditions and recommend the most economical conductor that still meets the requirement. .article-section table{display: table!important;} .article-section thead{display: table-header-group!important;} .article-section tbody{display: table-row-group!important;} .article-section tr{display: table-row!important;} .article-section th{display: table-cell!important;font-weight:bold;border:1px solid #cccccc;padding:8px;} .article-section td{display: table-cell!important;border:1px solid #cccccc;padding:8px;} .article-section caption{caption-side:bottom;font-size:16px;margin-bottom:12px;font-style:italic;color:#808080;} .article-section ol{margin-bottom:12px;list-style-type:decimal;list-style-position:inside;padding-left:0;} .article-section ul{margin-bottom:12px;list-style-type:disc;list-style-position:inside;} .article-section li{list-style:inherit;font-size:16px;margin-bottom:6px;} .article-section h2{font-size:22px;font-weight:bold;text-align:left;margin-bottom:12px!important;} .article-section h3{font-size:16px;font-weight:bold;text-align:left;margin-bottom:12px;} .article-section p{font-size:16px!important;margin-bottom:12px;} .product-card{display:block;margin:20px 0;border:1px solid #e5e7eb;border-radius:10px;overflow:hidden;font-style:normal;background:#fff} .pc-inner{display:flex;text-decoration:none;color:inherit;align-items:center;min-height:120px} .pc-img{width:160px;min-width:160px;aspect-ratio:4/3;height:auto;min-height:120px;object-fit:cover;flex-shrink:0;display:block;align-self:stretch} .pc-body{padding:12px 16px;flex:1;min-width:0;display:flex;flex-direction:column;align-self:stretch;justify-content:center} .pc-title{display:block;font-size:15px;font-weight:600;color:#111;margin:0 0 6px;line-height:1.4} .pc-desc{display:-webkit-box;font-size:13px;color:#6b7280;margin:0 0 8px;line-height:1.5;overflow:hidden;-webkit-line-clamp:2;line-clamp:2;-webkit-box-orient:vertical} .pc-cta{display:block;font-size:13px;font-weight:600;color:inherit;margin-top:auto} .pc-inner:hover .pc-title{text-decoration:underline} .article-section a:not(.pc-inner),article a:not(.pc-inner){color:inherit}.pc-cta{color:inherit!important}
-
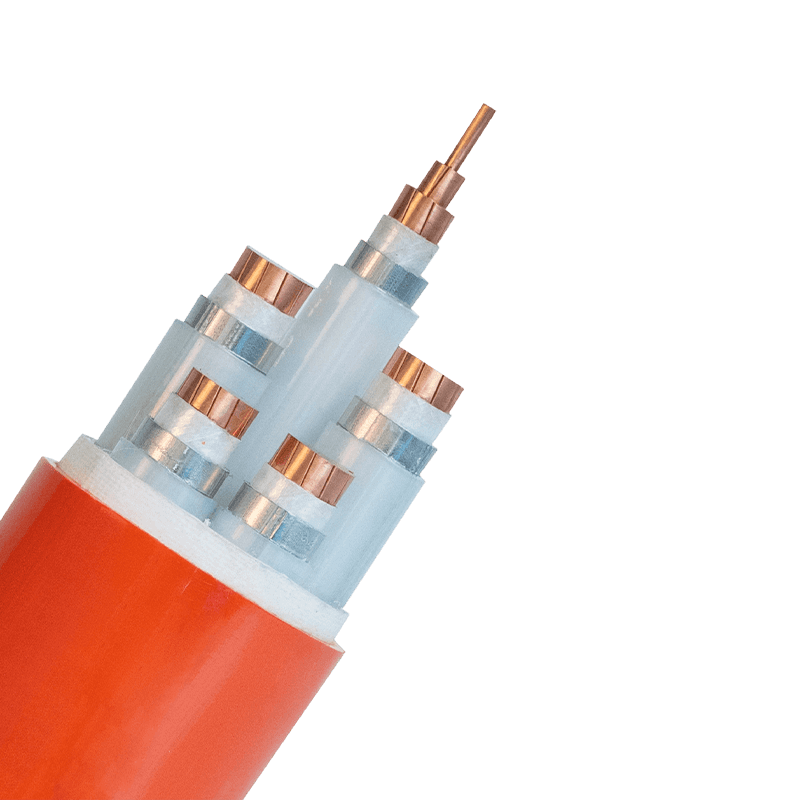 Flame-Retardant Cables: How They Work, Standards, and Selection Guide for BuyersOn a high-rise project, twenty floors of power and control cable often share a single vertical riser. Every meter of that cable is wrapped in polymer insulation — PVC, XLPE, rubber — and all of it is fuel. If a fire starts on one floor and the cable lets the flames travel up the bundle, the fire effectively climbs the building along its own wiring. This is the scenario flame-retardant cables are built for, and it is why serious tenders specify them by test standard rather than by a friendly adjective. The short answer: a flame-retardant cable is engineered to stop fire from spreading along the cable itself. It is not engineered to keep supplying power while the building burns — that is the job of fire-resistant cable, a different product tested to a different standard. Confusing the two either wastes money on circuits that never needed fire-rated construction or, far worse, leaves critical circuits dead at the exact moment they are needed most. The sections below cover how flame retardancy actually works, which standards govern it, how it differs from fire resistance, and how to match the right category to the way the cable will really be installed. What a Flame-Retardant Cable Is Designed to Do Across the industry, the working definition is deliberately blunt: a flame-retardant cable is one that will not convey or propagate flame beyond defined limits when tested. In a typical laboratory procedure, a standardized burner is applied to the cable — either a single sample or a whole bundle mounted on a vertical ladder — and then removed. The cable must self-extinguish within a fixed time, and the charred zone must stop below a set height. The numbers behind that definition matter more than the label. Under IEC 60332-3, a 3.5-meter bundle of cables burns in a vertical ladder tray, and the damaged portion must not extend more than 2.5 meters above the burner. The series is split into categories by how much non-metallic material the tray holds per meter: Category A (7 liters/m), Category B (3.5 L/m), Category C (1.5 L/m) and Category D (0.5 L/m), so a designer can match the test severity to the real density of the installation. In North America, UL 1685 (often cited together with IEEE 1202) covers vertical-tray fire spread and UL 1666 is the classic riser test; in the EU, EN 50575 makes fire performance a declared, CE-marked property of every cable intended for permanent installation in construction works. Why all this engineering for a cable? Because modern buildings carry enormous lengths of it, and a burning bundle behaves like a wick: rising heat, dripping molten insulation and fresh unburnt cable feeding in from below. Flame-retardant compounds are what break that loop, confining a small ignition to a small area instead of distributing it through the riser. Flame-Retardant and High-Temperature Resistant Wires and CablesFlame-Retardant Cables ManufacturersHigh-Temperature Resistant Wire and CableView Product → Flame-Retardant Is Not Fire-Resistant: The Difference That Decides the Spec Conclusion first: flame-retardant cable protects the building from the cable, while fire-resistant cable protects the circuit from the fire. A flame-retardant feeder that successfully self-extinguishes has still lost its insulation and its electrical continuity once flames reach it. If that feeder happens to serve a fire pump, a smoke-extraction fan, emergency lighting or a sprinkler control panel, losing the circuit during the fire itself is unacceptable — and that is precisely where codes require fire-resistant construction instead. Fire-resistant (fire-rated) cable is built and tested differently. IEC 60331 exposes the cable to a 750 °C flame for 90 minutes and requires the circuit to stay energized throughout, without short circuit or breakdown. BS 6387 goes further by adding water-spray (W) and mechanical-shock (Z) sequences on top of the fire-alone test (C). On the construction side there are two established routes: fire-resistant mica-glass tape wrapped over each conductor beneath the normal insulation, or true mineral insulated (MI) cable with a solid copper sheath and compressed magnesium oxide insulation that contains nothing combustible at all. Table 1. The two protections answer different engineering questions and are not substitutes for each other. Aspect Flame-retardant cable Fire-resistant cable Primary function Stop flame from propagating along the cable run Keep the circuit energized during the fire itself Governing tests IEC 60332 series, UL 1685/IEEE 1202, UL 1666, EN 50575 (CPR Euroclasses) IEC 60331, BS 6387, UL 2196 Behavior during a fire Cable self-extinguishes; the circuit may be lost Circuit remains live for the rated duration Typical applications General power, lighting, control and data runs in trays and risers Fire pumps, smoke extraction, emergency lighting, sprinkler controls, emergency power Mineral Insulated Fire-Resistant CablesMineral Insulated Fire-Resistant Cables ManufacturersMineral Insulated Fire-Resistant CablesView Product → Where Flame Retardancy Comes From: Halogenated vs. Halogen-Free Two chemistry routes dominate the market, and choosing between them is mostly a smoke question. The halogenated route Traditional halogenated designs use PVC compounds, usually with antimony trioxide added. When heated, the formulation releases chlorine species that interfere with the flame's radical chain reactions and promotes charring, so the cable quenches itself. It is economical and still widely used — but while it works, it emits hydrogen chloride, dense black smoke and corrosive gases, which endanger the people evacuating and corrode the electronics that survive the fire. The halogen-free route Halogen-free designs replace that chemistry with polyolefin or EVA compounds filled with aluminum trihydrate or magnesium hydroxide. Above roughly 200 °C, aluminum trihydrate releases chemically bound water in an endothermic reaction that cools the burning surface and leaves a stable, ceramic-like char. The cable still resists flame spread, but with little smoke and no corrosive halogen acid gas — the defining property of LSZH (low smoke zero halogen) designs. Smoke density is measured under IEC 61034, where many specifications demand at least 60% light transmittance, and halogen acid output is capped under the IEC 60754 series. For a fuller walkthrough of the labeling and standards, see our guide to what LSZH cables are and the fire-safety standards behind them. Tunnels, metro stations, airports, hospitals, data centers and high-rise escape routes are where low smoke earns its premium, because evacuation there depends on visibility and breathable air. Price-driven runs in ordinary, ventilated service spaces may not justify it. LSZH compounds generally cost more and can be slightly stiffer to bend, so blanket-specifying them everywhere is not automatically the safest or the cheapest engineering decision. Matching the Category to the Real Installation The most expensive mistake in this product family is buying a test result that does not match the installation. A cable that passes the single-cable test of IEC 60332-1 can still spread fire when installed twenty-deep in a ladder tray, because bundle geometry changes flame behavior completely. Specify by geometry instead: single drops in accessible spaces may legitimately rely on single-cable performance, while risers, dense trays and confined routes need bundled performance at a category matched to the expected cable volume. Regulatory context shapes the paperwork too. In the EU, EN 50575 folds fire performance into CE marking for construction cables, with CPR Euroclasses such as B2ca, Cca and Dca. In China, GB/T 18380 mirrors the IEC 60332 tests, designations ZA, ZB and ZC correspond to Category A, B and C behavior, and the WDZ prefix identifies low-smoke halogen-free constructions. A practical example from our own catalogue is WDZB1N-BYJ building wire, where WD marks low smoke and halogen-free, Z the flame-retardant function, B1 a defined burning-behavior grade and N fire-resistant performance — one construction carrying both protections for fixed building wiring. The classic demand points are high-rise risers, hospital and airport distribution, shopping-mall lighting and control, metro and rail-tunnel circuits and data-center pathways — in short, most of what modern building and infrastructure electrical installations contain. Building Wires for Fixed InstallationBuilding Wires ManufacturersCross-linked Polyolefin/PVC/Rubber Insulated Cable with Rated Voltage 450/750V and BelowView Product → A Procurement Checklist That Survives Review Before the purchase order goes out, run the specification through these six checks: Map the installation first: tray density, vertical runs and confinement decide whether single-cable or bundled-cable performance is required. Write the standard and category into the bill of quantities — "IEC 60332-3-24, Category C" — instead of the generic phrase "flame retardant," which invites the cheapest passing interpretation. Settle the halogen question explicitly: choose LSZH where evacuation visibility or sensitive electronics matter, and require the smoke and gas tests (IEC 61034, IEC 60754) on the same datasheet. Split the two protections deliberately: circuits that must stay live in a fire — fire pumps, smoke extraction, emergency lighting — get IEC 60331 or BS 6387 fire-resistant cable, not just stronger flame retardancy. Ask for type-test reports tied to the exact construction, conductor size and voltage rating; a certificate for a different design is decoration, not evidence. Check whether one combined construction — flame-retardant, low-smoke and fire-resistant — can replace stacked single-purpose cables; combined designs usually reduce tray congestion and total cost. Flame-retardant cable is a purchase where the specification language does most of the safety work. Keep the distinction clear — retardancy stops flame spread, resistance keeps the circuit alive — match the test standard to the real installation geometry, and verify every claim with reports rather than adjectives. Zhejiang Huapu Cable manufactures across the power, electrical-equipment, special and communication cable ranges, including flame-retardant and high-temperature-resistant constructions, mineral insulated fire-resistant cable and LSZH building wire. Our engineers work regularly with buyers and contractors who need a tender's fire-safety clauses translated into the right product with supporting test documentation, and we welcome drawings or specification extracts for exactly that kind of review. .article-section table{display: table!important;} .article-section thead{display: table-header-group!important;} .article-section tbody{display: table-row-group!important;} .article-section tr{display: table-row!important;} .article-section th{display: table-cell!important;} .article-section td{display: table-cell!important;} .article-section caption{caption-side:bottom;font-size:16px;margin-bottom:12px;font-style:italic;color:#808080;} .article-section th{font-weight:bold;border:1px solid #cccccc;padding:8px;} .article-section td{border:1px solid #cccccc;padding:8px;} .article-section ol{margin-bottom:12px;list-style-type:decimal;list-style-position:inside;padding-left:0;} .article-section ul{margin-bottom:12px;list-style-type:disc;list-style-position:inside;} .article-section li{list-style:inherit;font-size:16px;margin-bottom:6px;} .article-section h2{font-size:22px;font-weight:bold;text-align:left;margin-bottom:12px!important;} .article-section h3{font-size:16px;font-weight:bold;text-align:left;margin-bottom:12px;} .article-section p{font-size:16px!important;margin-bottom:12px;} .product-card{display:block;margin:20px 0;border:1px solid #e5e7eb;border-radius:10px;overflow:hidden;font-style:normal;background:#fff} .pc-inner{display:flex;text-decoration:none;color:inherit;align-items:center;min-height:120px} .pc-img{width:160px;min-width:160px;aspect-ratio:4/3;height:auto;min-height:120px;object-fit:cover;flex-shrink:0;display:block;align-self:stretch} .pc-body{padding:12px 16px;flex:1;min-width:0;display:flex;flex-direction:column;align-self:stretch;justify-content:center} .pc-title{display:block;font-size:15px;font-weight:600;color:#111;margin:0 0 6px;line-height:1.4} .pc-desc{display:-webkit-box;font-size:13px;color:#6b7280;margin:0 0 8px;line-height:1.5;overflow:hidden;-webkit-line-clamp:2;line-clamp:2;-webkit-box-orient:vertical} .pc-cta{display:block;font-size:13px;font-weight:600;color:inherit;margin-top:auto} .pc-inner:hover .pc-title{text-decoration:underline} .article-section a:not(.pc-inner),article a:not(.pc-inner){color:inherit}.pc-cta{color:inherit!important}
Knowledge sharing
-
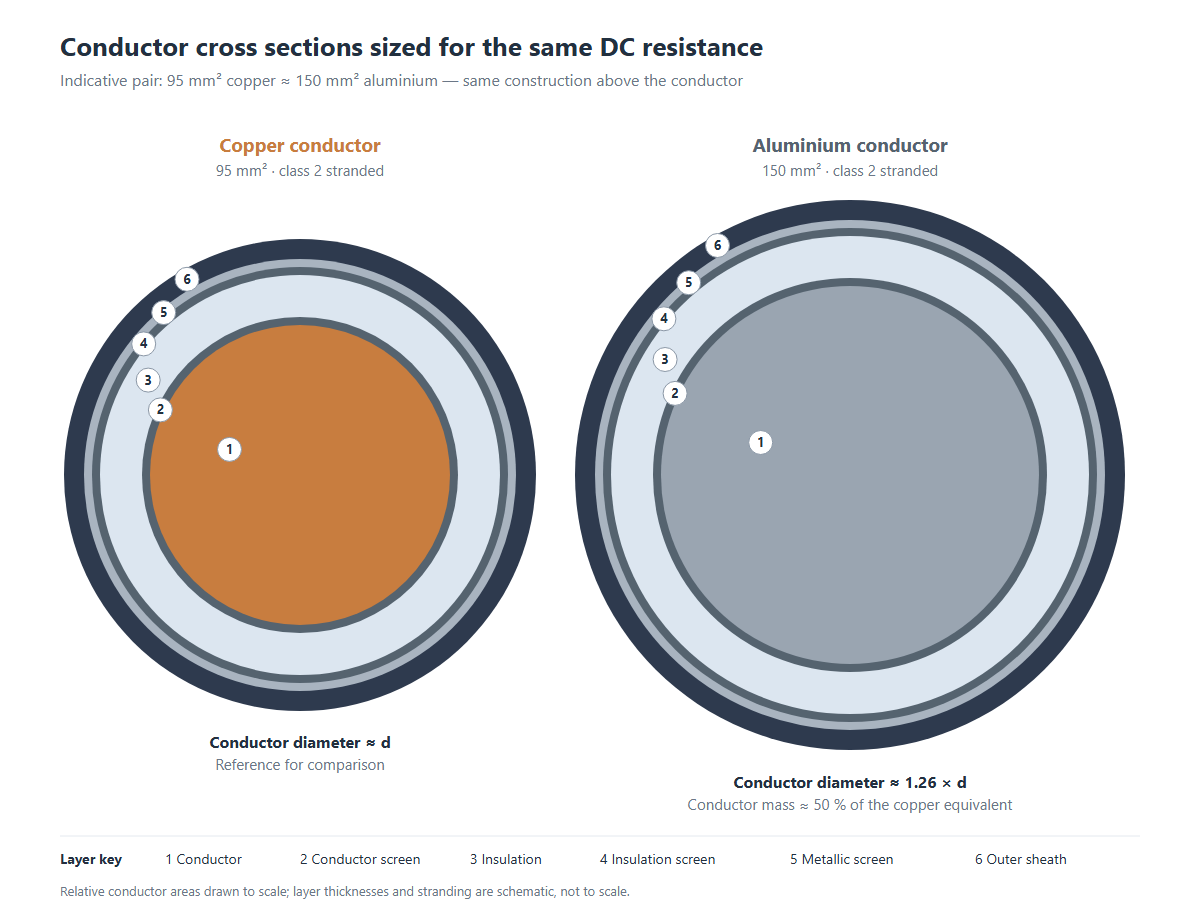 Copper vs Aluminium Conductor The Real Cost Comparison for MV Projects
-
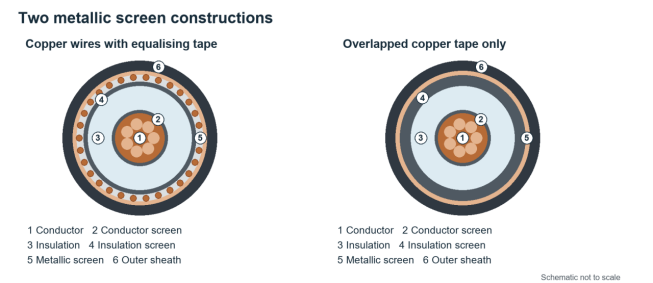 Copper Wire and Tape Shield vs Copper Tape Shield in MV Cables
-
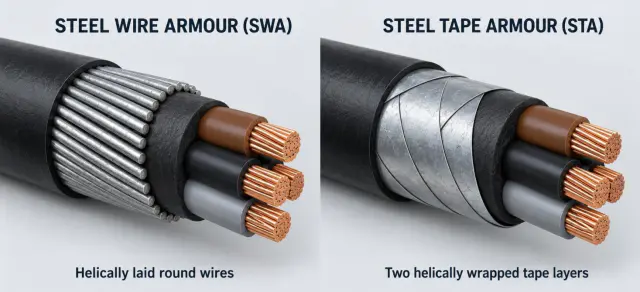 Steel Wire vs Steel Tape Armour in Power Cables
-
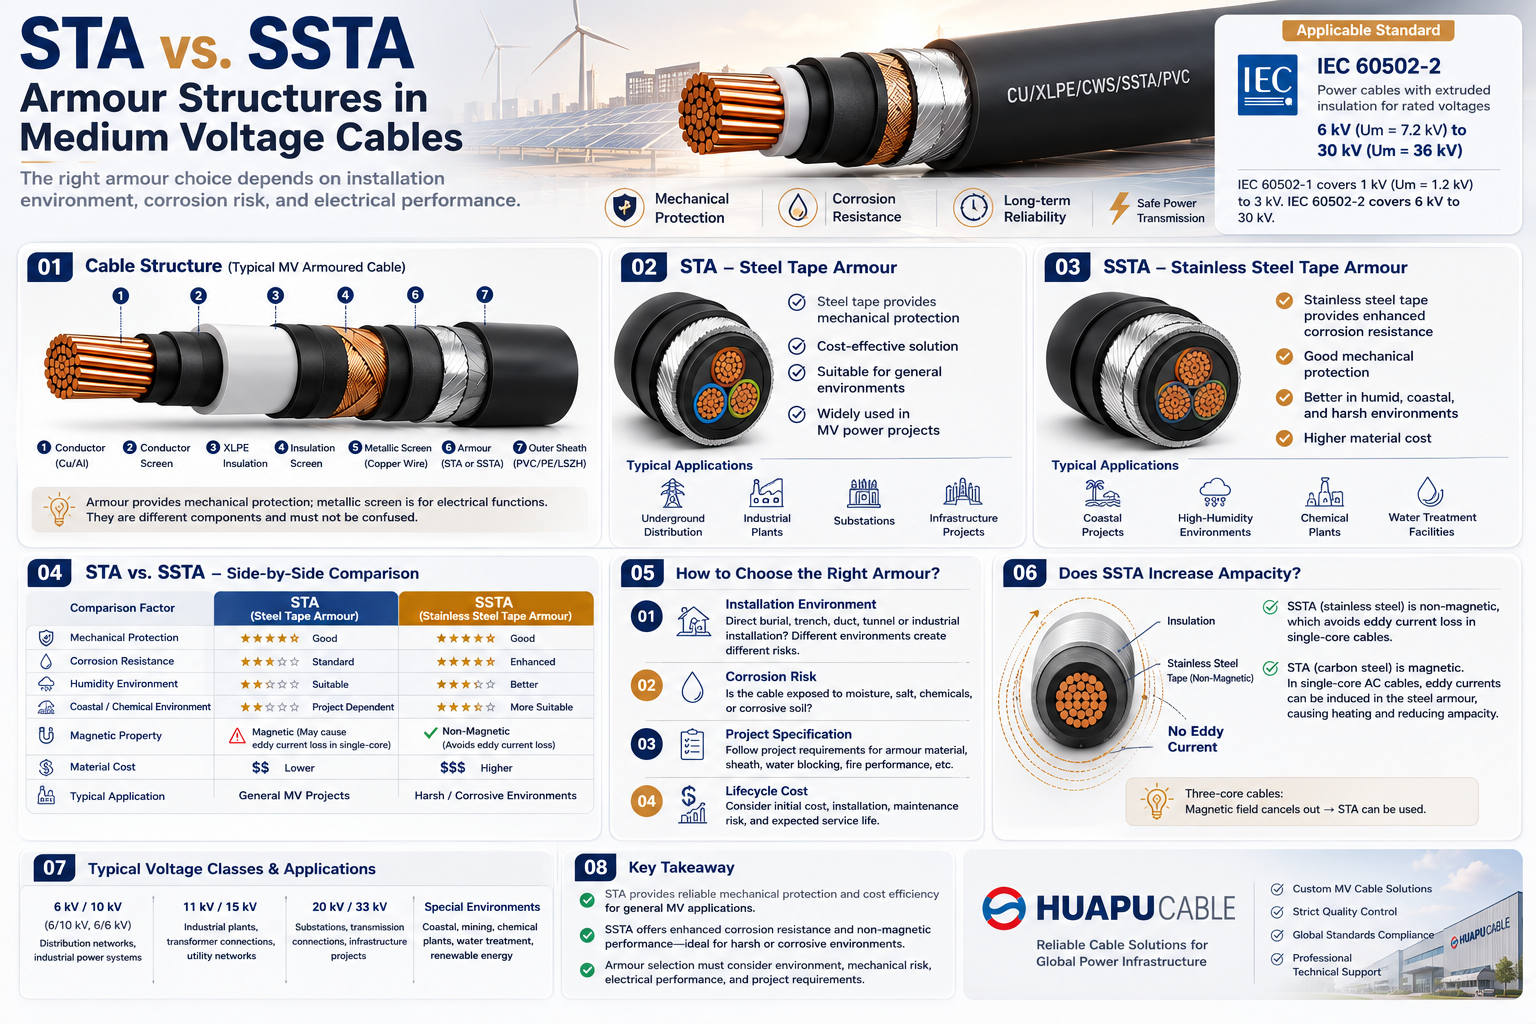 STA vs. SSTA Armour: Structure and Applications in Medium Voltage Cables
-
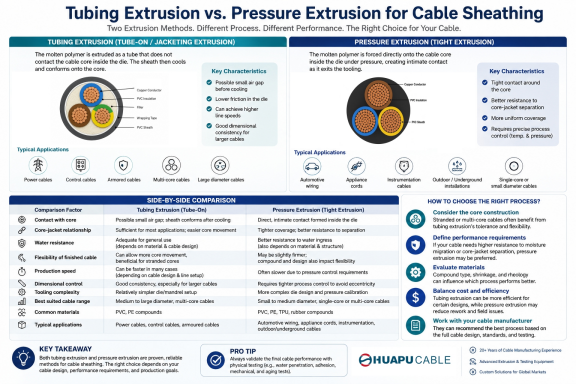 Tube Extrusion vs. Pressure Extrusion Cable Sheathing: A Practical Comparison Guide
Our Email
Our Tel
- +86-13588204183
Our Address
- No. 39 Zhiyuan Road, Deqing Economic Development Zone, Huzhou City, Zhejiang Province
QR Code
Quick Links
Online Message
Copyright © Zhejiang Huapu Cable Co., Ltd. All Rights Reserved.
 ISO 9001 Cable Manufacturer